The previous two notes covered molding and surface finishing. This one steps half a pace back, to the operation between demolding and inspection: flash removal.
In many workshops that is still "tear it off by hand". Silicone is soft and flash is thin, so it looks like it comes away easily — until you make visible parts or seals and discover that how cleanly it tears depends entirely on how the flash was designed and which way it is pulled. Then volume grows, someone proposes a cryogenic trimmer "like the rubber factory uses", and an easily missed premise appears: silicone does not go brittle.
So this note is not a machine recommendation. It separates the operation into its parts: why silicone behaves differently, what each route can actually achieve, and which parts should be fixed in the tool rather than in post-processing.
1. The premise: a very low glass transition
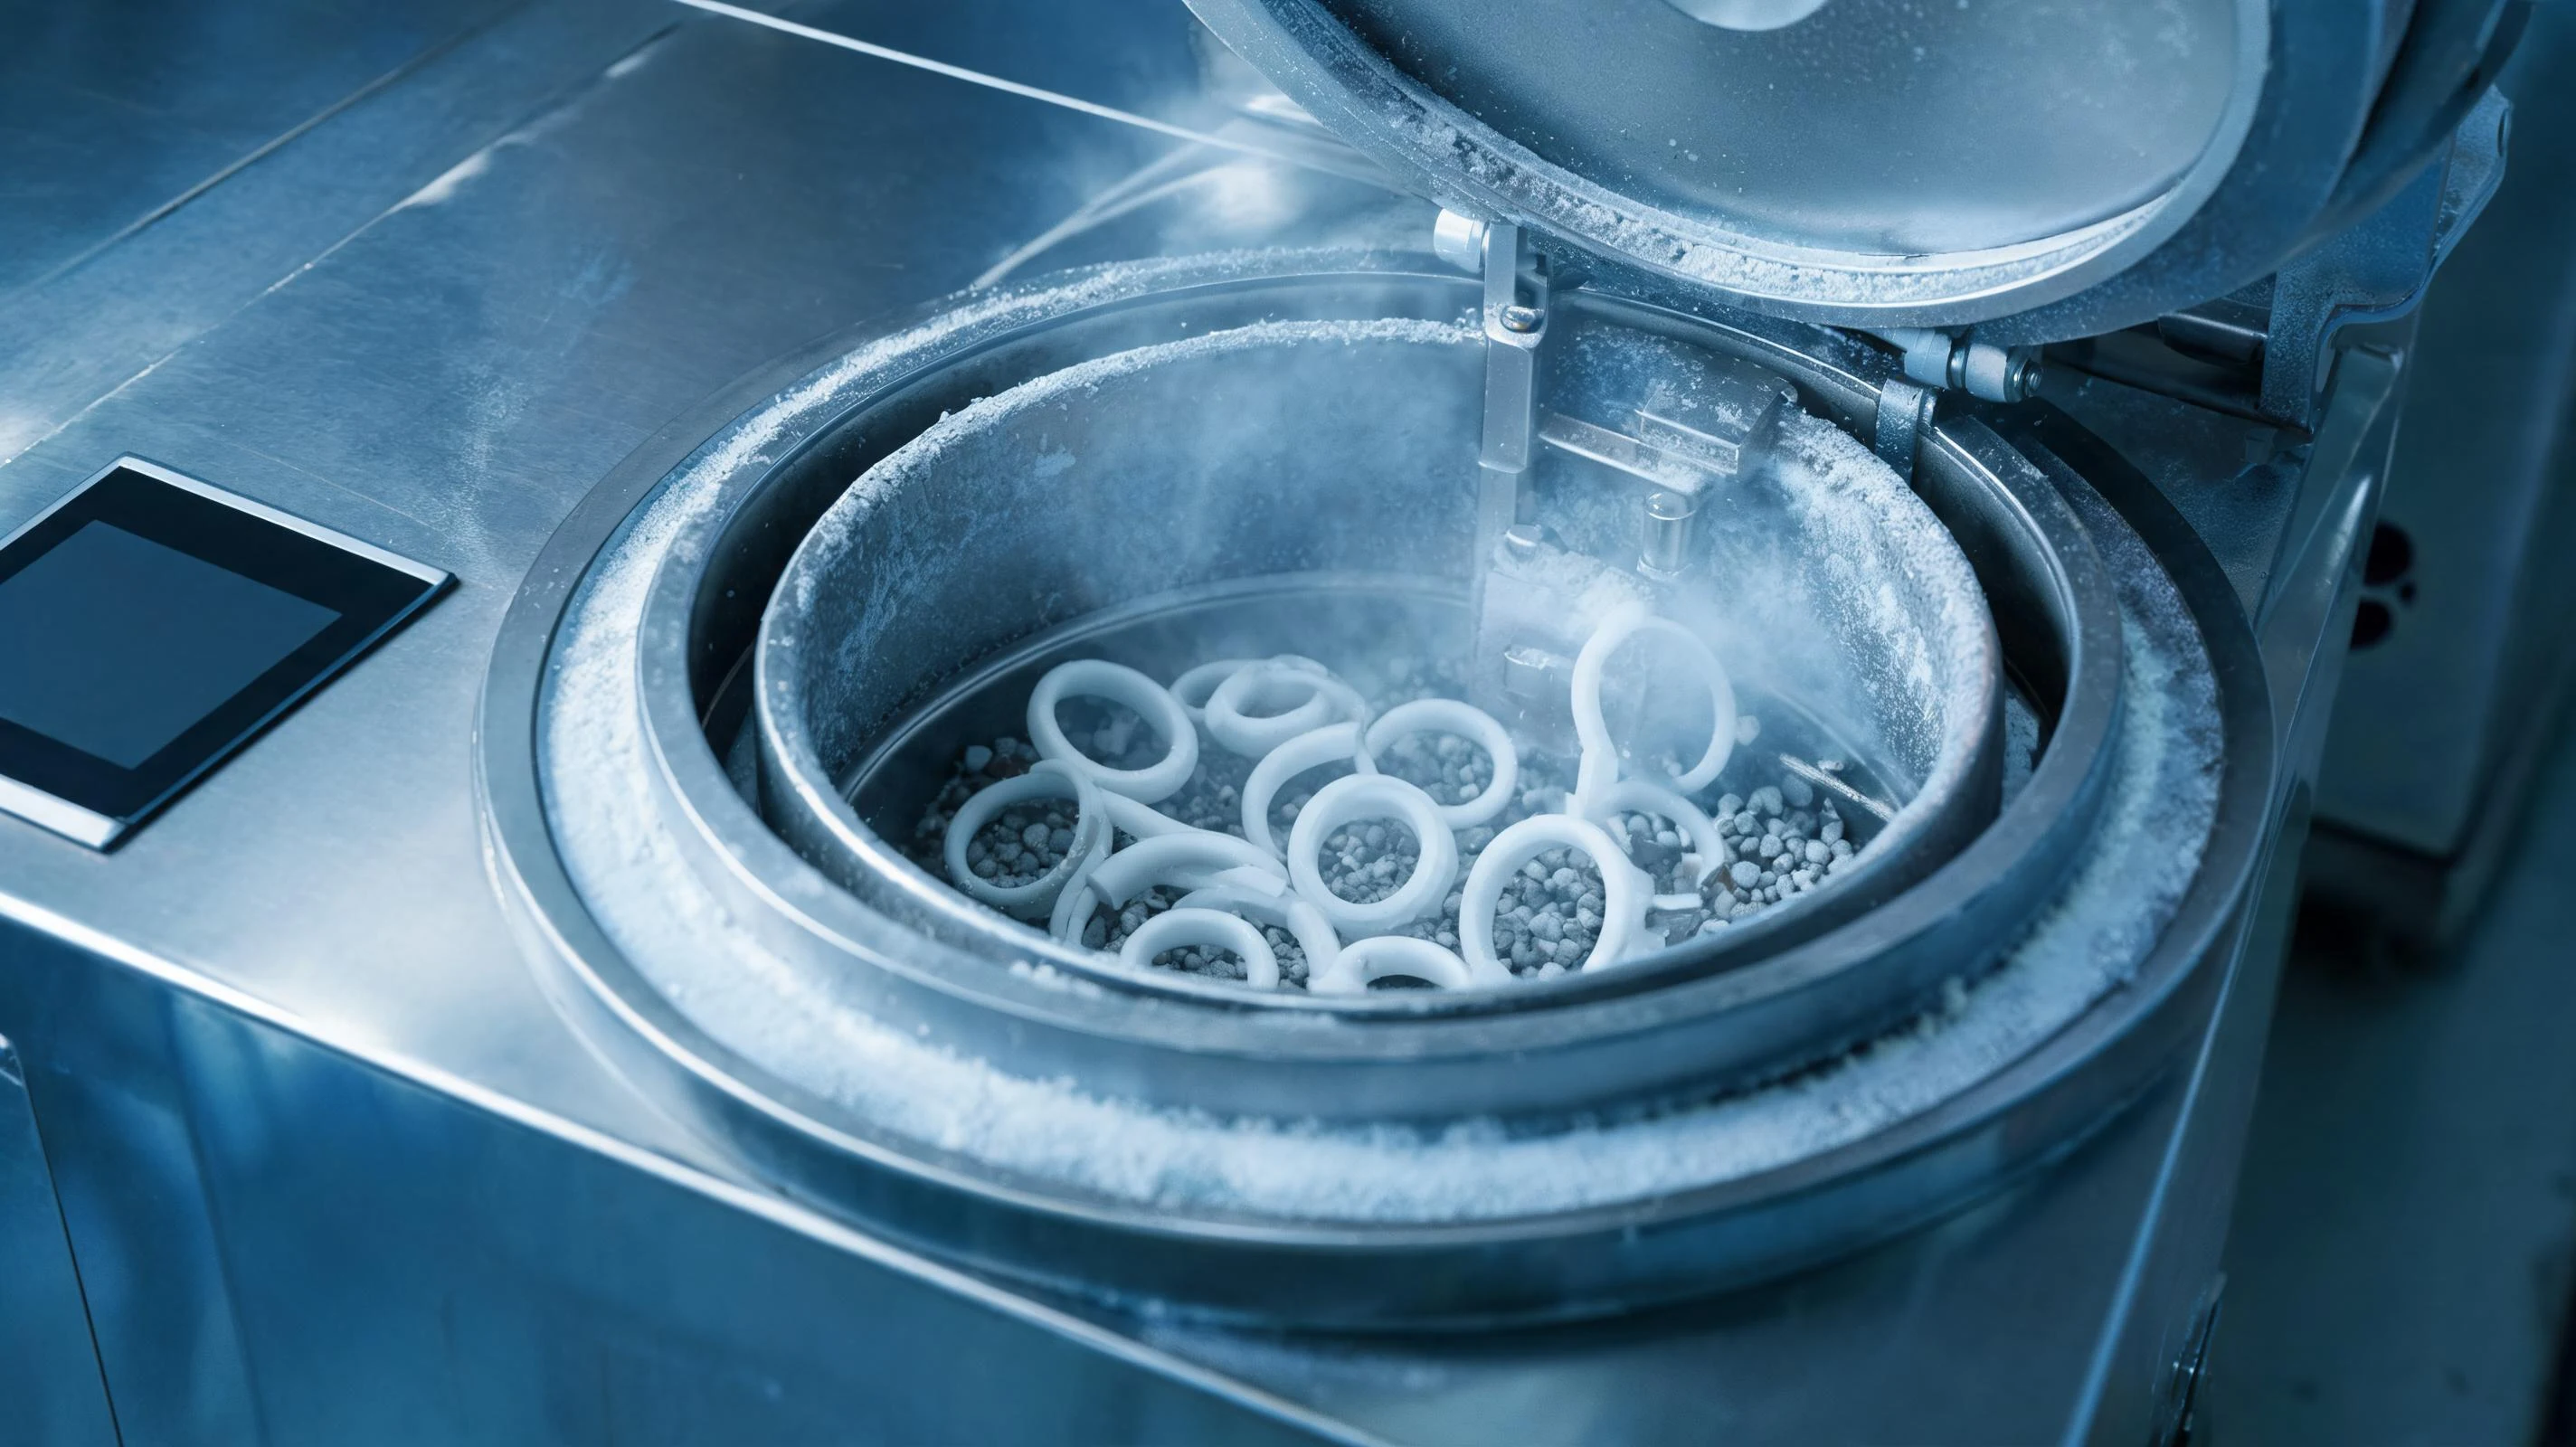
Cryogenic trimming cools parts below their glass transition so flash embrittles, then blasts it off with media. It is mature for NBR and EPDM, whose glass transition sits roughly between -40 °C and -60 °C — an ordinary cold chamber takes the flash out of its elastic range.
Silicone is different. The PDMS backbone has a glass transition near -125 °C, so at a chamber temperature of -80 °C the part is still elastic: media hits the flash and it bounces back rather than breaking off. That is not a machine setting problem; it is the material.
Three responses exist in the industry: push the temperature lower, extend the cycle with media rubbing, or design the flash so it breaks at a defined root. The third is usually the most effective and the cheapest, because it happens at the tooling stage.
2. Three things that make silicone flash different
- Low glass transition: it will not embrittle; cold mainly reduces elasticity, it does not turn flash into glass.
- Low tear strength: an advantage and a risk. Flash breaks cleanly at the root, but once a tear starts it runs along the edge — serrations, nicks, and sometimes a tear into the sealing lip.
- Thin and surface-hugging: typically 0.05–0.15 mm, growing flush against the parting line. Pull direction, grip point and speed all change the fracture, which is why two operators trim the same batch differently.
So the logic is not "cut it off" but: design the fracture + control pull direction and allowance + local mechanical or media treatment + a written acceptance standard. Miss one and you get "looks clean, leaks when assembled".
3. The cheapest step: remove flash in the tool
- Parting-line flatness and mould rigidity: poor flatness, weak plates or badly placed support pillars open under clamp force and thicken the flash. Thick flash is hard to tear and drags the part's radius with it.
- Tear-trim geometry: a sharp step or a very thin neck at the flash-to-part boundary concentrates stress so flash breaks at the root. Done well, it improves manual trimming consistency and makes automation feasible.
- Venting and vacuum: trapped gas lifts the parting line and creates local thick flash; vacuum-assisted molding reduces it noticeably.
- Shot size and metering: overshoot pushes excess compound into the parting line. Precision metering and cold-runner control do more than save material here.
- Tool maintenance: release-agent residue, cured build-up and rust thicken flash and glue it into the cavity, so trimming tears the part. Fix the cleaning interval and coating condition.
Get these right and flash becomes thin, continuous and flush — the precondition for any post-processing route to work reliably.
4. Four post-processing routes, and what each can do
Manual trimming is the most flexible and the most operator-dependent: small batches, odd geometries, cosmetic parts, or already-thin flash. Consistency depends on feel; cuts and nicks are hard to avoid; labour cost keeps rising. Its value is handling what others cannot, not being cheap.
Cryogenic trimming (liquid nitrogen plus media impact) usually runs as a drum or carousel with polycarbonate, urea or walnut-shell media from a fraction of a millimetre to about 1.5 mm. It is mature for NBR and EPDM; for silicone it needs longer cycles, lower temperature and harder media — closer to cold tumbling than to brittle fracture.
Dry-ice blasting and high-pressure water jets are non-contact and can be positioned precisely. Water jets commonly run at 1000–3000 bar and handle cross-holes, blind holes and internal cavities; the drawbacks are drying and nozzle path control. Dry ice sublimates and leaves no media, but watch for condensation marks and static-attracted dust.
Force-controlled robotic brushing with vision follows the edge and suits local flash, complex outlines and cosmetic parts. Silicone is soft: a little too much pressure dents it or grinds a chamfer, so force accuracy and path compensation decide success — and cycle time usually depends on fixturing, not robot speed.
| Route | Best-fit parts | Consistency | Risk to silicone | Volume threshold | Cost basis |
|---|---|---|---|---|---|
| Manual trimming | Small batches, odd shapes, cosmetic parts, very thin flash | Low, operator-dependent | Scratches, nicks, uneven edge | None | Labour per piece |
| Cryogenic trimming | Complex small parts with blind holes, stable volumes | Medium-high once parameters are locked | Thin walls distorted by overcooling, micro-cracks, slight whitening | Relatively high, continuous running | LN2 + media + machine depreciation |
| Dry ice / water jet | Cross-holes, internal cavities, local flash, parts that cannot be loaded | High with a fixed path | Water marks and condensation, thin edges damaged by the nozzle | Medium | Media and energy + drying step |
| Robot force-controlled brushing | Local flash, cosmetic requirements, complex outlines | High with vision and force control | Denting from excess force, chamfers ground in | Medium to high | Fixtures + programming + upkeep |
5. Five parameters that actually matter in a cryogenic chamber
- Temperature: chambers and media commonly run between -60 °C and -120 °C. Chasing lower temperatures adds LN2 cost and distorts thin walls while gaining little elasticity loss.
- Cycle time: several short cycles usually beat one long freeze; overall overcooling costs rebound, which seals notice.
- Media: size, hardness and shape drive removal rate. Worn media loses efficiency, so inspect and top up by batch.
- Load: overloaded drums scratch parts against each other and shield flash; underloaded ones waste the cycle.
- Unloading and warm-up: condensation leaves marks on cosmetic parts and static pulls media dust onto surfaces; ionised air and a warm-up zone matter more than expected.
One boundary is not a parameter: parts thinner than 1 mm, softer than Shore A40, or with very sharp cosmetic edges are poor candidates. The typical symptom of overcooling is not leftover flash but a broken edge — visible under a loupe, yet a leak or a different feel once assembled.
6. Judgement: what counts as "clean"
The weakest link is rarely the machine but the standard. An executable standard states at least four things: the residual flash limit (length and thickness, not "no flash"), the over-trim boundary (nicks, flattened radii, out-of-tolerance dimensions — scrapped once the sealing lip is touched), the surface condition (scratches, haze, whitening, water marks, separate for cosmetic and structural parts), and the sampling versus 100% inspection split.
Vision inspection helps, but transparent, black and very soft parts are the hardest: flash is close in colour to the part, reflections are weak, and clamping can deform it. Backlighting, multiple angles and go/no-go gauges usually carry the decision.
7. Automation: do the accounting first
Count three blocks together: direct cost (depreciation, LN2 or water, media, fixtures, maintenance), quality cost (over-trim scrap, rework, complaints — a seal that fails because of trimming costs far more than the labour saved), and changeover plus flexibility (fixture commonality, time to switch). Slow changeover kills automation in high-mix, low-volume work.
In practice, stable high volumes, complex geometry and a written standard are the projects that pay back; high-mix, low-volume cosmetic work still does better with skilled hands and a better tool.
8. Checklist for tooling and process
- Has parting-line flatness, plate rigidity and pillar layout been checked against clamp deflection?
- What flash thickness is the target, and can the current tool hold it?
- Are tear-trim position, edge sharpness and flash allowance defined so the fracture lands outside the part radius?
- Is venting or vacuum assistance needed, and will vents clog?
- Is shot size or metering overshooting, and is the cold runner stable?
- Are release-agent use and cleaning intervals fixed, with no build-up in the cavity?
- Do hardness, wall thickness and cosmetic requirements fall outside the "not for cryogenic" range?
- Are residual-flash and over-trim limits written down, with who judges and with what tool?
- Is the sampling plan and the 100% inspection list for critical features clear?
- Can changeover time and fixture commonality support the current order mix?
Conclusion
Treat deflashing as a manual finishing step and the cost hides in rework and complaints; treat it as a design outcome and most of the problem disappears at tooling. Silicone not going brittle is a useful reminder: rather than chasing a colder chamber, get the tear-trim, the parting line and the venting right, then let post-processing do what it is good at — breaking an already-designed fracture cleanly.
If you have parts with stubborn flash, inconsistent trimming or an automation decision to make, send the geometry, hardness, flash thickness and batch size. We will tell you whether the fix belongs in the tool or in post-processing.